


Press release
Certified PP EVOH Barrier Sheet From China: How Multilayer Technology Is Extending Fresh Food Shelf Life
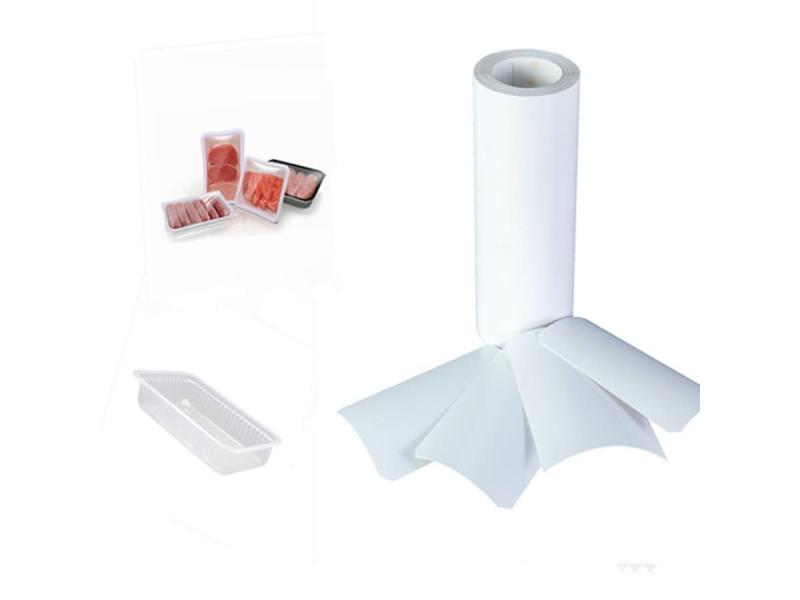
Certified PP EVOH Barrier Sheet From China: How Multilayer Technology Is Extending Fresh Food Shelf Life
The Molecular Anatomy of EVOH: Intercepting Oxygen Permeation at the Crystalline Level
To understand how advanced multi-layer packaging prevents oxidation, one must examine the polymer chemistry of Ethylene Vinyl Alcohol, commonly known as EVOH. This copolymer consists of polymerized ethylene and vinyl alcohol units, which combines excellent melt processability with exceptional gas barrier properties. On a molecular scale, the highly polar vinyl alcohol segments form extremely strong, cohesive hydrogen bonds. These powerful intermolecular forces create a dense, highly crystalline polymer matrix. When oxygen molecules attempt to penetrate this crystalline structure, they encounter a highly tortuous path. This physical maze slows down gas diffusion to negligible rates, virtually blocking oxygen entry into the food package. However, EVOH exhibits a unique thermodynamic vulnerability that engineers must address during design. Because of its polar hydroxyl groups, EVOH has a high affinity for water molecules. When exposed to high-humidity environments, moisture easily penetrates the polymer matrix and disrupts the intermolecular hydrogen bonding. This swelling action increases molecular mobility and significantly degrades the oxygen barrier performance. Consequently, packaging designers cannot use EVOH as a standalone monolayer in moist or chilled food environments. To protect its structural integrity, engineers must encapsulate the EVOH layer between protective hydrophobic polymer barriers. This strategic placement ensures that the core barrier layer remains dry and highly effective under challenging distribution conditions.
The Multilayer Symphony: Engineering the PP/EVOH/PP Co-Extrusion Architecture
To overcome the moisture sensitivity of EVOH, advanced manufacturers utilize co-extrusion technology to create a symmetrical five-layer sheet structure. This complex configuration places the EVOH barrier in the center, flanked by protective adhesive layers and durable outer polymers. The exterior layers consist of Polypropylene, or PP, which exhibits excellent hydrophobic properties and high structural rigidity. Polypropylene acts as an outstanding shield against water vapor transmission, keeping the internal EVOH layer completely dry. Therefore, the internal EVOH core maintains its maximum gas barrier efficiency even when storing high-moisture foods like fresh poultry. However, combining polar EVOH with non-polar PP requires specialized chemical compatibility solutions. Because these polymers do not naturally bond, co-extrusion lines must introduce thin adhesive tie layers between them. These modified polyolefin resins chemically bond with both PP and EVOH, preventing delamination during subsequent processing. Delamination is a critical failure point during secondary operations such as high-temperature thermoforming or vacuum sealing. If the layers separate, the structural integrity of the container fails, and oxygen immediately enters the package. By optimizing the adhesive formulation and extrusion temperature, manufacturers ensure permanent mechanical bonding. This mechanical cohesion allows the PP EVOH PP packaging film(https://www.fullstarxm.com/pp-evoh-pp-packaging-film-for-food-preserve_p39.html) to withstand deep-draw thermoforming without losing its barrier properties. Consequently, food processors receive a robust packaging material that performs reliably under extreme physical stresses.
Quantifying the Preservation Margin: Empirical Data on OTR and WVTR Reductions
Material scientists evaluate barrier performance using two primary metrics: Oxygen Transmission Rate, or OTR, and Water Vapor Transmission Rate, or WVTR. Measuring these rates provides clear empirical evidence of the superiority of multilayer co-extruded sheets over traditional packaging options. For instance, standard monolayer PP sheets exhibit relatively high OTR values, often exceeding one hundred cubic centimeters per square meter per day. This high rate allows oxygen to penetrate the package quickly, limiting fresh meat shelf life to just a few days. In contrast, a high-barrier PP/EVOH/PP sheet reduces the OTR to less than two cubic centimeters. This represents an incredible decrease in gas permeation, shielding the food from oxidative degradation. Similarly, the outer PP layers maintain the WVTR at extremely low levels, preventing product dehydration and weight loss. In real-world applications, this scientific barrier performance translates directly to extended preservation margins. Fresh beef, which typically spoils within four days in standard packaging, can maintain freshness for up to fourteen days under modified atmosphere conditions. Seafood products also benefit from extended color stability and delayed bacterial growth. For retailers, these quantitative improvements reduce in-store waste, optimize inventory management, and expand geographical distribution limits.
Certified Excellence: How Xiamen Fullstar Translates Polymer Science into Food-Grade Reliability
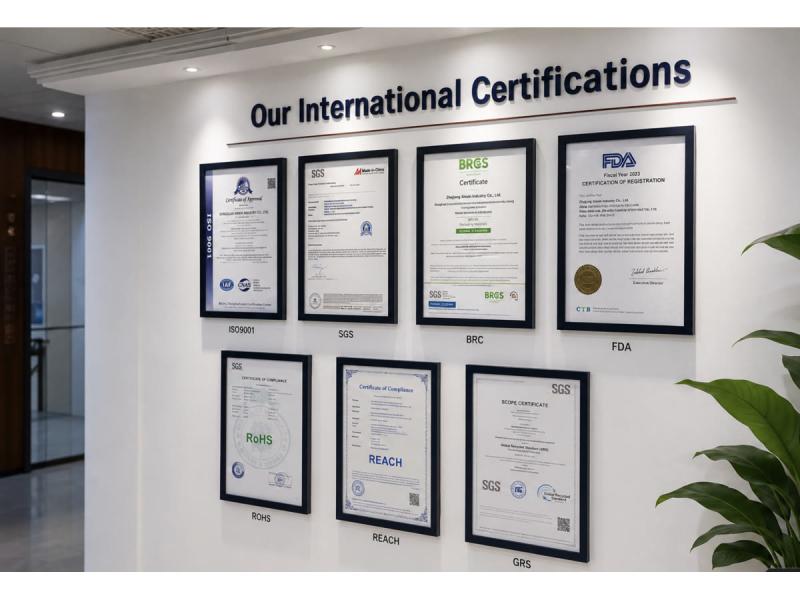
Translating advanced polymer science into reliable commercial products requires exceptional manufacturing expertise and strict quality assurance. In the global packaging market, Fullstar(Xiamen Fullstar Imp.&Exp.Trading Co.,Ltd.)(https://www.fullstarxm.com/about-us_d1) serves as a premier manufacturer of high-barrier materials. The enterprise possesses sophisticated multi-layer co-extrusion production lines that ensure precise layer thickness control. Maintaining an even distribution of the EVOH barrier across the entire sheet is essential for consistent protection. Even a tiny thin spot can compromise the entire package and lead to localized food spoilage. To prevent this, Fullstar utilizes advanced automated scanning systems to monitor sheet thickness in real-time. Furthermore, Xiamen Fullstar Imp.&Exp.Trading Co.,Ltd. produces materials that comply fully with rigorous international food safety regulations, including FDA and BRC standards. Their clean production facilities and raw material traceability protocols guarantee that no harmful substances migrate into the food. In addition to standard specifications, the technical team at the company designs customized barrier formulations to meet specific client needs. For example, some food items require higher heat resistance for retort sterilization, while others need maximum clarity for retail presentation. By adjusting the polymer ratios, the technical team optimizes the physical characteristics for diverse applications. Ultimately, this engineering precision allows global food processors to deliver safe, high-quality products to consumers. Through these continuous technological innovations, the global supplier remains a trusted partner for modern sustainable food logistics. Discover more about these advanced co-extruded barrier sheets and explore the complete product line at the official corporate website: https://www.fullstarxm.com/.
Unit301,Jinlong Road NO.889, Jimei District, Xiamen City, Fujian Province, China
Xiamen Fullstar Imp.&Exp.Trading Co.,Ltd.
Fullstar
fullstar@xmfullstar.com
+86 18259239846
FULLSTAR is a professional manufacturer and supplier of plastic sheets with over 20 years of industry experience. Starting in 2003 as a distributor of PVC sheets from Nan Ya Plastics in Taiwan, the company also distributes various new types of sheets and films from Nan Ya. It is also the largest distributor of PET sheets in China, in partnership with Far Eastern Group. As a diversified industrial and trading group, we provide one-stop solutions from design and R&D to production, and hold multiple international certifications including ISO 9001, BRC, RoHS, and REACH.
Housed in modern, dust - free facilities, our factory features 4 dedicated production lines for PP/HIPS sheets and 4 for PET, achieving a monthly capacity of 2,000 tons. Additionally, Our equipped with 3 automatic thermoforming production lines, specialize in custom solutions like MAP trays for large - scale clients-engineered to meet unique specifications. In 2026, we established an overseas factory in Malaysia to provide customers with more stable supply channels and access to the European and American markets.We maintain over 10 sets of material testing systems to ensure consistent quality and reinforce partnerships through exceptional after - sales support.
Our extensive product range includes high - quality PP, PET, and HIPS sheets, PP synthetic paper, and various plastic products. These serve diverse sectors such as food packaging, electronics, crafts blister packaging, labels, and printing.
Partner with Fullstar for all your plastic sheet needs-where decades of expertise, rigorous certifications, and customer - driven innovation unite to deliver tailored solutions.
This release was published on openPR.
Permanent link to this press release:
Copy
Please set a link in the press area of your homepage to this press release on openPR. openPR disclaims liability for any content contained in this release.
You can edit or delete your press release Certified PP EVOH Barrier Sheet From China: How Multilayer Technology Is Extending Fresh Food Shelf Life here
News-ID: 4660687 • Views: …
More Releases from Xiamen Fullstar Imp.&Exp.Trading Co.,Ltd.
Why China Leading PSU Core Tube Suppliers Are Redefining Reverse Osmosis System …
The 2026 Industrial Benchmark: Why Modern Membrane Systems Demand Advanced Core Materials
Industrial water treatment systems face unprecedented performance demands in the year 2026. Global regulatory bodies have tightened standards for zero liquid discharge and industrial wastewater recycling across all major manufacturing sectors. Consequently, desalination plants, chemical facilities, and power generation stations must push their filtration systems to maximum operational capacity. Spiral-wound membrane elements serve as the primary defensive line against…
Top 5 Questions to Ask Before Choosing a Certified Food Grade PP Sheet Supplier …
Global food brands face extreme pressure regarding safety compliance. Regulatory agencies strictly monitor plastic packaging materials to prevent consumer health hazards. Microscopic chemical leaching remains a primary concern during long-distance transportation and extended storage. Therefore, packaging managers must select their material vendors with extreme care. Finding a reliable Certified Food Grade PP Sheet Supplier(https://www.fullstarxm.com/0-2mm-2mm-food-grade-high-transparent-polypropylene-pp-plastic-sheet-for-vacuum-forming_p127.html) represents a critical step in protecting corporate reputation. Certified plastic sheets do not simply act as…
The Complete Buyer's Guide to Reliable ED Membrane Stack Suppliers for Industria …
The High-Salinity Challenge: Demanding Electrochemical Precision in Industrial Zero-Liquid Discharge Projects
Industrial wastewater management faces intense regulatory scrutiny across the globe in 2026. Heavy industries must implement reliable systems to achieve Zero-Liquid Discharge goals and protect local ecosystems. Traditional thermal evaporation systems demand massive capital expenditures and consume excessive amounts of fossil fuels. Similarly, standard reverse osmosis systems fail when handling highly saturated brine streams due to severe membrane fouling. To…
ISO 9001 to BRC: What Certifications Matter When Sourcing High Quality Double Co …
The Global Compliance Mandate: Why Certificates Dictate Operational Risk in Multi-Layer Sourcing
Global logistics and packaging procurement require immense operational discipline in 2026. Global brands must protect their product integrity and navigate complex regulatory landscapes across different continents. Standard administrative checks no longer suffice when evaluating international polymer suppliers. Instead, corporate auditors rely heavily on third-party certifications to filter out high-risk manufacturing partners. When procurement teams look for reliable polymer extrusion…
More Releases for EVOH
Ethylene Vinyl Alcohol Copolymer Evoh Evoh Resin Market Analysis By Application, …
The Ethylene Vinyl Alcohol Copolymer Evoh Evoh Resin Market reached a valuation of 5.76 billion in 2025 and is anticipated to expand at a CAGR of 8.62% during the forecast period from 2026 to 2033, ultimately attaining an estimated value of 11.17 billion by 2033. Market growth is being driven by increasing demand across industrial, commercial, and technology-oriented applications, supported by ongoing innovation, expanding application areas, and rising investments across…
Ethylene-Vinyl Alcohol Copolymer (EVOH) Films Market 2023-2030
Global Ethylene-Vinyl Alcohol Copolymer (EVOH) Films Market Set for Growth Driven by Packaging Industry Expansion:
The global market for Ethylene-Vinyl Alcohol Copolymer (EVOH) films is witnessing substantial growth, fueled by the escalating demand in the packaging industry. EVOH, known for its crystal-clear, flexible, and glossy properties, serves as a robust barrier material, particularly effective in packaging food, cosmetics, medications, and perishable items. The market analysis conducted by [Your Company], based on…
High Barrier Material (PVDC, EVOH, PEN) Market 2022 | Detailed Report
ReportsnReports publishes the report titled High Barrier Material (PVDC, EVOH, PEN) that presents a 360-degree overview of the market under one roof. The report is developed with the meticulous efforts of an enthusiastic and experienced team of experts, analyts, and researchers that makes the report a valuable asset for stakeholders to make robust decisions. This report also provides an in-depth overview of product type, specification, technology, and production analysis considering…
PEX-EVOH Pipe Market Size, Share, Development by 2024
LP INFORMATION offers a latest published report on PEX-EVOH Pipe Market Analysis and Forecast 2019-2025 delivering key insights and providing a competitive advantage to clients through a detailed report.
According to this study, over the next five years the PEX-EVOH Pipe market will register a xx% CAGR in terms of revenue, the global market size will reach US$ xx million by 2024, from US$ xx million in 2019. In particular,…
PEX-EVOH Pipe Market Size, Share, Development by 2024
Global Info Research offers a latest published report on PEX-EVOH Pipe Market Analysis and Forecast 2019-2025 delivering key insights and providing a competitive advantage to clients through a detailed report. This report focuses on the key global PEX-EVOH Pipe players, to define, describe and analyze the value, market share, market competition landscape, SWOT analysis and development plans in next few years.
To analyze the PEX-EVOH Pipe with respect to individual growth…
EVOH for Packaging Market
Introduction and Need of the Product:
EVOH, also termed as Ethyl Vinyl Alcohol Copolymer, is a high oxygen barrier material which is widely used for the perishable food packaging applications. It is commonly used as a barrier film in the prevailing flexible and rigid packaging formats such as pouches, bags, etc. through the co-extrusion process, to protect food items from oxygen ingress. Widespread use of the EVOH barrier material shifted the…

