


Press release
Fin Forming Equipment Selection Gains Attention Among Global Buyers
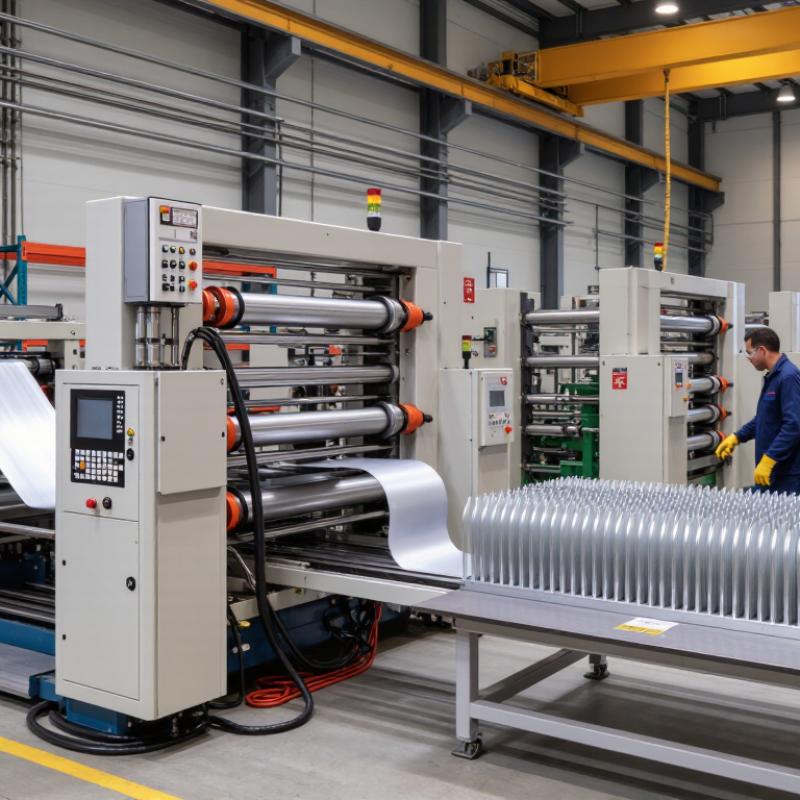
Now, he wasn't a fin-machine seller, but his point rings true for any equipment decision. Good results come from thorough testing, crystal-clear specs, and careful evaluation of suppliers. Don't just take their word for it-ask for samples run with your actual materials. Check the fin height, how consistent the pitch is, burr formation, and how quickly you can switch over. And remember, it's not just about how fast the machine outputs - look at scrap rates too.Those little details? They can end up costing you a lot if overlooked.For global buyers, it's also smart to consider things like tooling support, operator training, spare parts availability, electrical standards, and how fast remote service can happen.
A machine that's perfect for one factory might not match the skills or maintenance routines of another. Plus, language barriers can slow down troubleshooting. And don't forget about shipping damage - that can be a real headache right out of the box. All of these risks should be given some serious thought before you hit 'buy.'In the end, choosing equipment shouldn't just be about the lowest price tag. It's about the overall value over its lifetime-energy consumption, tooling and maintenance costs, downtime, calibration needs, and how flexible it is for future product changes. Some folks still get caught up in chasing maximum speed, but honestly, I'd say stable quality often delivers more real value than just going for the fastest cycle times.This guide is all about helping you compare Fin Forming Equipment with more confidence. The focus is on proven performance, the credibility of the supplier, hands-on experience, and honestly, the sometimes uncomfortable gap between what's promised and what you see happening on your factory floor.
Image: https://ecdn6.globalso.com/public/img/2026-09-22/95b3212901030a39d1f856ba5f793200.png
Define Fin Types: Plate-Fin, Louvered-Fin, and Fin Densities Above 20 FPI
When choosing fin forming equipment, define the fin type before comparing machine capacity. Plate-fin cores use flat or lightly corrugated sheets stacked with separators. They suit compact heat exchangers and require accurate plate feeding, fin-height control, and clean cutting. Louvered-fin designs use angled openings to disturb airflow and improve heat transfer. Their forming tools need stable pitch, sharp louver edges, and controlled strip tension. A small tooling error can create uneven airflow.Fin density above 20 FPI needs closer attention. Higher density can increase surface area, but it may also raise air resistance and complicate forming. For example, 24 FPI aluminum stock needs consistent roll pressure and reliable lubrication control. During equipment trials, inspect fin pitch, louver angle, strip flatness, and burr formation. Do not judge performance from speed alone. A fast machine with unstable feeding creates expensive scrap. I have seen trial parts pass visual inspection but fail after stacking. That mistake is easy to repeat.Tips: Ask for sample runs using your actual alloy, thickness, fin height, and target FPI. Check whether operators can adjust pitch without lengthy changeovers. Measure finished fins with calibrated gauges, not visual estimates. Leave room for improvement. Your first density choice may be technically correct but commercially inefficient. Verify thermal results, pressure drop, maintenance access, and spare tooling before approving the equipment.
How to Choose Fin Forming Equipment for Global Buyers? - Define Fin Types: Plate-Fin, Louvered-Fin, and Fin Densities Above 20 FPI
EVALUATION DIMENSION
PLATE-FIN HEAT EXCHANGER
LOUVERED-FIN HEAT EXCHANGER
EQUIPMENT AND PURCHASING CONSIDERATIONS
Basic Fin Structure
Flat or corrugated fins are layered between separator plates. The fin creates extended surface area and supports compact, multilayer heat-transfer cores.
Thin fins contain angled louvers that interrupt the boundary layer and increase air-side heat transfer. The fin is commonly used in compact air-cooled cores.
Specify the fin geometry, material thickness, pitch, louver angle, and required dimensional tolerances before selecting a forming machine.
Typical Fin Density
Common compact-core designs may use approximately 10-40 FPI, depending on the fluid, allowable pressure drop, and cleaning requirements.
Common automotive and compact air-side designs may use approximately 14-30 FPI. Designs above 20 FPI require tighter control of strip feeding and fin height.
FPI means fins per inch. For densities above 20 FPI, confirm the machine's minimum pitch, feed accuracy, tooling stability, and repeatability at production speed.
Heat-Transfer Behavior
Provides a broad range of thermal performance. Offset, wavy, or serrated plate fins can improve turbulence and surface efficiency.
Louvers generate repeated flow interruption and can provide high air-side heat transfer in a relatively shallow core depth.
Use validated thermal design data rather than fin density alone. Higher FPI does not automatically produce better total exchanger performance.
Air-Side Pressure Drop
Usually moderate, but pressure drop rises as fin density, fin length, and flow velocity increase.
Often higher than a plain-fin design at the same frontal area because the louvers increase flow disturbance and wetted surface interaction.
Match the equipment output to the fan or blower duty. Require pressure-drop targets at the specified air temperature, mass flow, and altitude.
Resistance to Dust and Fouling
Lower-density plate-fin configurations are generally easier to clean and less likely to block quickly than very dense fin packs.
Fine louver passages can collect dust, fibers, insects, or oily deposits, especially when the louver pitch is small.
For dusty or oily service, evaluate washable coatings, fin spacing, access for cleaning, filtration, and the long-term effect of blockage on pressure drop.
Manufacturing Process
Typical processes include roll forming, corrugating, cutting, stacking, brazing, soldering, or mechanical assembly, depending on the core design.
Typical processes include fin rolling, louver slitting or stamping, forming, cutting, and subsequent tube-and-fin or plate-and-fin assembly.
Ask whether the supplier can provide the complete process route, including decoiling, lubrication, forming, cut-to-length control, scrap handling, and inspection.
Tooling Requirements
Tooling is selected for fin profile, wave height, pitch, strip width, and material thickness. Changeover may require forming rolls or corrugating tools.
Tooling must control louver angle, louver length, louver pitch, fin height, and cut pattern. Louver tooling is generally more sensitive to wear and alignment.
Compare tool-change time, tool life, spare-part availability, adjustment methods, and whether one machine platform supports multiple FPI ranges.
Material Compatibility
Common materials include aluminum alloys, copper, stainless steel, and other formable alloys selected for thermal, corrosion, and mechanical requirements.
Common materials include aluminum and copper alloys; the selected alloy must maintain sufficient ductility during louvering and fin-height forming.
Confirm material temper, yield strength, thickness range, coil width, surface treatment, and compatibility with lubricants and joining methods.
High-Density Forming Above 20 FPI
Feasible when the forming rolls, guides, and cutting system maintain consistent pitch and fin height without crushing or buckling the strip.
Feasible, but the narrow louver and fin geometry increases the need for precise synchronization, stable strip tension, and sharp, correctly aligned tooling.
Request production samples at the target FPI, not only at a lower density. Inspect pitch variation, fin height, louver opening, burrs, waviness, and crushed sections.
Dimensional Quality
Key checks include fin pitch, fin height, wave or serration profile, strip width, cut length, flatness, and core stacking accuracy.
Key checks include fin pitch, fin height, louver angle, louver length, opening condition, cut length, flatness, and tube-to-fin fit.
Define inspection methods and sampling frequency. Digital calipers, optical measurement, profile gauges, and first-article inspection can support quality control.
Best-Fit Applications
Compact heat exchangers, refrigeration cores, process equipment, electronics cooling, gas-to-gas exchangers, and applications requiring varied fin profiles.
Radiators, condensers, charge-air coolers, HVAC coils, oil coolers, and other forced-air applications where high air-side performance is important.
Select based on fluid type, air velocity, allowable pressure drop, contamination level, required compactness, and serviceability-not on the fin name alone.
Production Flexibility
Often suitable for multiple fin profiles and core arrangements when the line supports interchangeable forming rolls and adjustable guides.
Suitable for repeat production of defined louver patterns; flexibility depends strongly on the number of available louver and pitch tool sets.
For global buyers, compare the number of supported specifications, changeover procedure, recipe storage, operator training, and remote technical support.
Energy and Operating Factors
Energy demand depends on strip thickness, material strength, line speed, forming load, and downstream joining process.
Additional louver-forming work can increase forming load and tool wear compared with simple flat-fin production.
Evaluate installed power, compressed-air demand, lubrication consumption, line speed at target quality, and expected maintenance intervals.
Recommended Buyer Decision
Choose when the project needs adaptable fin profiles, a broader range of core configurations, or easier access and cleaning at moderate fin density.
Choose when compact air-side performance is a priority and the operating environment permits the additional fouling and pressure-drop risk.
Before purchase, provide drawings, target FPI, material data, coil dimensions, output requirement, sample standards, utilities, applicable safety rules, and acceptance criteria.
Buyer note: Fin density is only one design variable. Final equipment selection should be verified through thermal calculations, pressure-drop analysis, material trials, sample production, and a documented factory acceptance test at the intended operating range.
Specify Aluminum Grades: 3003 and 4343/3003 Clad for Heat-Exchanger Fins
Choosing fin forming equipment starts with the aluminum grade, not the machine catalogue. For standard heat-exchanger fins, 3003 aluminum offers good formability and stable corrosion resistance. It suits louvered, wavy, and plain fin designs. The equipment should control strip tension carefully. Small tension changes can distort narrow fin channels.4343/3003 clad aluminum requires more attention. The 3003 core provides strength, while the 4343 layer supports brazing during heat-exchanger assembly. Buyers should confirm clad ratio, temper, thickness tolerance, and surface condition before selecting a forming line. Roll tooling must avoid scratches on the clad surface. Lubrication should also support clean brazing later. Do not assume every fin machine handles clad strip equally well.Practical trials reveal details that brochures often miss. Check louver height, pitch accuracy, burr formation, and strip tracking at production speed. Measure samples after forming, not only before it. A stable line should maintain quality across different coil widths and batch changes. Operators also need clear controls and accessible tooling adjustments. One common mistake is choosing maximum speed too early. Speed is useful, but repeatable fin geometry matters more. The specification may still need revision after trial runs. That is normal. Request material certificates, inspection records, and traceability documents for every coil. This supports reliable purchasing across regions.
How to Choose Fin Forming Equipment for Global Buyers?
Specify Aluminum Grades: 3003 Core and 4343/3003 Clad for Heat-Exchanger Fins
The chart shows representative alloying-element ranges in weight percent from commonly used AA/EN composition specifications. Aluminum 3003 is typically selected for the fin core, while 4343 is used as the brazing-clad layer in 4343/3003 sheet. Equipment should be matched to the selected strip thickness, clad ratio, temper, and forming requirements.
Calculate Line Capacity from Stroke Rates of 60-300 Strokes per MinuteHow to Choose Fin Forming Equipment for Global Buyers?
Stroke rate is the starting point for estimating fin line capacity. A press running at 60 strokes per minute produces 3,600 strokes per hour. At 300 strokes per minute, the theoretical figure reaches 18,000 strokes. The practical formula is:
output = strokes per minute times 60 times fins per stroke times availability times yield.
For example, one fin per stroke, 85% availability, and 90% yield produce about 2,754 to 13,770 acceptable fins per hour. The calculation changes sharply when tooling forms several fins in one stroke.
Do not select equipment from speed alone. Feed pitch, strip thickness, fin height, stroke length, material hardness, and changeover time affect real capacity. A 300-stroke line may require slower operation when aluminum strip bends unevenly or scrap rises. World Steel Association reported 1.89 billion tonnes of crude steel production in 2023, showing the scale of global metal demand, but that figure does not guarantee stable forming performance. ISO 6892-1 testing principles can help verify material strength before final line sizing. My experience is that a clean spreadsheet often looks more confident than the factory floor.
Tips: Record hourly output for several shifts, not one trial. Measure downtime, scrap, and tool adjustments separately. Leave a 10-15% capacity margin for maintenance and material variation. If the buyer needs 10,000 good fins per hour, a machine rated at exactly 10,000 strokes may be too small. Calculate with real yield. Recheck it.
Match Material Thicknesses from 0.05-0.30 mm to Press Accuracy Requirements
Choosing fin forming equipment starts with material thickness, not machine size. For 0.05-0.10 mm strip, tiny feeder errors can distort pitch and create uneven fin height. Use a guided press with low vibration, closed-loop feed control, and stable die alignment. A practical target is feed repeatability within plus-minus 0.02 mm, but the die design and material temper may demand tighter control.For 0.10-0.20 mm material, many production lines can use a high-speed mechanical press with precise shut height adjustment. At 0.20-0.30 mm, forming force rises, and frame stiffness becomes more important than headline speed. Keep an eye on burr height, springback, and strip flatness. ASTM B557 testing principles and ISO 2768 tolerance guidance can support inspection planning, although they do not replace a product-specific drawing.Market scale also affects equipment decisions. The World Steel Association reported 1.89 billion tonnes of crude steel production in 2023, while the International Aluminium Institute reported about 70.6 million tonnes of primary aluminium output. These figures show broad material availability, but supply consistency still varies by alloy and temper. A neat spreadsheet can mislead. Trial the actual coil. Record thickness variation, hardness, lubrication, and pitch stability. For ultra-thin stock, I would rather accept a slower press with better repeatability than chase speed and repair damaged dies. That preference is not universal. It should be tested against scrap rate, maintenance access, and the buyer's inspection capability.
Compare Servo, Mechanical, and Roll-Forming Systems by Energy and Output DataHow to Choose Fin Forming Equipment for Global Buyers?
Energy and output must be measured together. The U.S. Department of Energy's Manufacturing Energy Consumption Survey reports machine drive consumes about 23% of U.S. manufacturing energy. That figure makes motor efficiency important, but it does not predict every forming line's cost.
23%
Servo systems draw power mainly during active movement. They can reduce idle losses and recover energy during deceleration. Output is flexible, with programmable stroke depth and timing. This suits varied fin pitches and frequent changeovers. Mechanical presses usually deliver higher fixed-speed output. Their flywheel stores energy efficiently during repeated strokes, but it continues consuming power during idle periods. Roll-forming systems run continuously. Typical production speeds often range from 20 to 60 meters per minute, depending on material thickness, profile, and cutting method.
Measure the real cycle.
A useful comparison records kilowatt-hours per 1,000 finished fins, not motor nameplate power. It also records rejects, setup minutes, and line speed. The European Commission's Best Available Techniques Reference Document for Metal Processing stresses process control and energy monitoring as practical efficiency tools.
However, published savings can mislead. My own evaluation would separate warm-up, idle, forming, and cutting energy. A servo machine may win on mixed production, while a mechanical press may outperform it on long, stable runs. Roll forming can achieve excellent output, but tooling alignment becomes critical. One wrong guide can create meters of scrap before operators notice.
Verify Global Compliance with CE, ISO 9001, and 400-480 V Power Standards
Choosing fin forming equipment for global production requires more than comparing output rates. Electrical and quality compliance can decide whether a machine starts safely on arrival. Check the CE documentation carefully, including the Declaration of Conformity, risk assessment, and applicable directives. The documents should match the exact machine model. A copied certificate is not enough.
ISO 9001 shows that the manufacturer operates a documented quality management system. It does not automatically prove that every machine is reliable. Verify the certificate scope, issuing body, validity dates, and production site. Ask for inspection records, calibration evidence, and test results from a comparable fin forming line. Factory experience matters here. Small details, such as guarded rollers, labeled control cabinets, and clear emergency stops, often reveal more than polished sales material.
Power compatibility deserves equal attention. A specification marked 400-480 V may still require confirmation of frequency, phase configuration, tolerance, grounding, and startup current. Ask whether the control system accepts the local supply directly. Otherwise, a transformer or electrical modification may be required. Check it early. A checklist helps, but it can create false confidence. I have seen buyers verify voltage while overlooking connector types and site earthing. That mistake is avoidable. Request wiring diagrams, installation requirements, and a pre-shipment inspection before approving delivery.
Conclusion
Choosing the right Fin Forming Equipment requires a clear understanding of the fin design, material, capacity, precision, and compliance requirements. Buyers should first identify whether they need plate-fin or louvered-fin production, especially when working with fin densities above 20 FPI. Aluminum grades such as 3003 and 4343/3003 clad are commonly suited to heat-exchanger applications, while material thicknesses from 0.05 to 0.30 mm must be matched with suitable press accuracy and tooling stability.Production planning should also consider stroke rates between 60 and 300 strokes per minute to ensure that line capacity meets demand. Servo, mechanical, and roll-forming systems can be compared through their energy consumption, operating speed, maintenance needs, and output consistency. Finally, global buyers should verify CE and ISO 9001 compliance, as well as compatibility with 400-480 V power standards, to support reliable installation, safe operation, and consistent performance across international production environments.
About Us
SMAC Intelligent Technology Co., Ltd.
Founded in 2010 and located in Nantong Economic Development Zone, SMAC Intelligent Technology Co., Ltd. specializes in manufacturing equipment for the global heat exchange industry, including fin press lines, hairpin benders, coil expanding machines, straight tube cut-offs, return U benders, ring loading machines, and related robots and automation solutions.
Media Contact
Company Name: SMAC INTELLIGENT TECHNOLOGY CO.,LTD
Contact Person: Media Relations
Email:Send Email [https://www.abnewswire.com/email_contact_us.php?pr=fin-forming-equipment-selection-gains-attention-among-global-buyers]
Country: China
Website: https://www.smacitc.com/
Legal Disclaimer: Information contained on this page is provided by an independent third-party content provider. ABNewswire makes no warranties or responsibility or liability for the accuracy, content, images, videos, licenses, completeness, legality, or reliability of the information contained in this article. If you are affiliated with this article or have any complaints or copyright issues related to this article and would like it to be removed, please contact retract@swscontact.com
This release was published on openPR.
Permanent link to this press release:
Copy
Please set a link in the press area of your homepage to this press release on openPR. openPR disclaims liability for any content contained in this release.
You can edit or delete your press release Fin Forming Equipment Selection Gains Attention Among Global Buyers here
News-ID: 4640071 • Views: …
More Releases from ABNewswire
Susan Kay "Susie" Kimes, Christian Ministry Pioneer and Founder of NEWIM and Cho …
Susan Kay "Susie" Kimes, founder of NEWIM and Chosen Women Events, died September 15, 2026, at age 79. A pioneering Christian women's ministry leader, mentor, and spiritual mother, she devoted her life to Jesus, family, discipleship, generosity, and helping others. Her legacy continues through SusanKimesLegacy.com.
MENIFEE, CA - September 22, 2026 - Susan Kay "Susie" Kimes, a pioneering leader in Christian women's ministry, founder of the Network of Evangelical Women in…
Dukas: China Top Comprehensive Screw Air Compressor Manufacturer Driving Industr …
LINYI CITY, SHANDONG PROVINCE, CHINA - September 22, 2026 - Against the backdrop of surging global energy costs and accelerating industrial decarbonization, compressed air systems - often called the "fourth utility" of modern manufacturing - are undergoing a profound technological upgrade. As factories worldwide prioritize energy savings, operational reliability and total cost of ownership, Chinese manufacturers have emerged as pivotal players in the global screw compressor landscape. Standing at the…
7 Key Tips for Choosing an N Male 4GHz 200W Load for RF Applications
Hefei City, Anhui Province, China - September 22, 2026 - Picking out a N-Male 4GHz 200W load isn't just about matching the connector and checking the power rating, you know? In RF testing, tiny gaps in specs can lead to pretty big measurement errors. Sure, a load might look perfect on paper, but during real continuous use, it can heat up way faster than you'd expect or just not perform…
Bone Filling Mesh Containers Gain Attention as Medical Needs Evolve in 2026
Jinan, Shandong Province, China - September 22, 2026 - Picking out a Bone Filling Mesh Container in 2026 isn't just about glancing at pictures or comparing prices. There's so much more to consider since the right container really impacts how well the graft stays in place, how easy it is to handle, how clear the surgical view remains, and how stable the whole reconstruction ends up. For instance, a tiny…
More Releases for Fin
Longitudinal Fin Tubes in Tank Heating
In petrochemical, fine chemical, grain and oil processing, new energy and other industries, storage tanks are core equipment for medium storage. The efficiency and stability of their heating systems directly affect production efficiency, product quality and operating costs.
Traditional tank heating mostly uses bare tube heat exchange components, which generally suffer from low heat transfer efficiency, slow heating, high energy consumption and easy fouling and blockage. Especially when handling viscous…
Fintelligence (Fin-telligence.com) Reviews Silver Prices
In this article, Fintelligence reviews the surge in silver prices, highlighting how industrial demand and supply constraints have contributed to the metal's record high.
As silver prices continue to rise, traders, especially those in the Netherlands, are closely monitoring these developments.
The current market conditions offer potential opportunities, but a thorough understanding of the key factors driving silver's growth is essential for anyone looking to invest or trade in this…
Fin Types for Aluminum Plate Fin Heat Exchangers
1: Definition of Aluminum Fins [https://www.coolerchina.com/]
Fins are the most basic components of plate-fin heat exchangers. The heat transfer process is mainly completed by fins, and only a part is completed directly by the partition.
The connection between the fins and the partition is perfect brazing, so most of the heat is transferred to the cold carrier through the fins and the partition.
Since the heat transfer of the fins [https://www.coolerchina.com/] is not…
Fin Fish Market Prolific Business Methodology and Techniques and Revenue | Cooke …
Fin Fish Market size reached US$ 186.1 Billion in 2022. Looking forward, the market to reach US$ 242.4 Billion by 2028, exhibiting a growth rate (CAGR) of 4.3% during 2023-2028. Feeding, production, regular stocking, and conservation of aquatic life are all part of the production and fishing of fin fish. Freshwater, brackish, and marine waters are the three environments in which fin fish are raised. In addition, freshwater aquaculture is…
Fin Fish Market Progresses for Huge Profits by 2027 : Marine Harvest ASA, P/F Ba …
Major players in the industry have adopted strategies such as acquisition, partnership & agreement, merger, and geographical expansion, to expand their market share and increase profitability. The key player in the market include Cermaq Group AS (Mitsubishi Corporation), Cooke Fin fish Inc., Grupo Farallon Fin fish, Leroy Sea Food Group, Marine Harvest ASA, P/F Bakkafrost, Selonda Fin fish S.A., Stolt Sea Farm, Tassal Group Limited, and Thai Union Group Public…
High Frequency Welded Fin Tubes market: New Prospects to Emerge by 2028 | Delfin …
"The global High Frequency Welded Fin Tubes Market is carefully researched in the report while largely concentrating on top players and their business tactics, geographical expansion, market segments, competitive landscape, manufacturing, and pricing and cost structures. Each section of the research study is specially prepared to explore key aspects of the global High Frequency Welded Fin Tubes Market. For instance, the market dynamics section digs deep into the drivers, restraints,…

