
Press release
Sheet Metal Bend Relief: Types, Design Rules and Size Guidelines
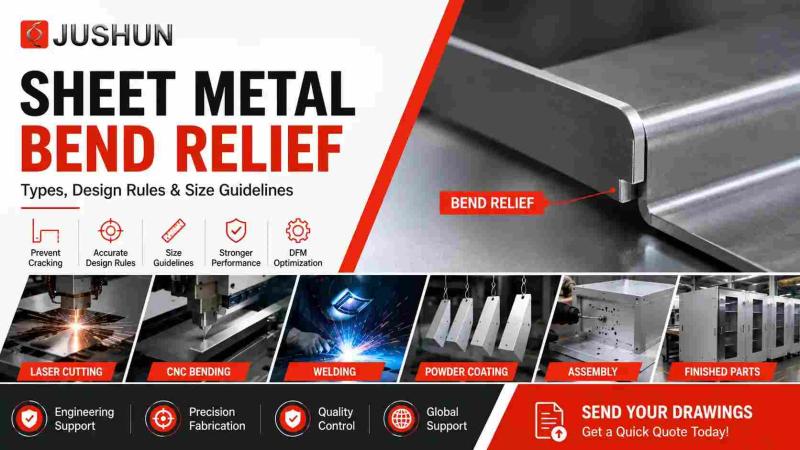
Bend relief design isn't just a detail-it's critical to preventing leaks and failures in sheet metal fabrication.
https://www.jushunmetal.com/blog/sheet-metal-bend-relief/
The purpose is to reduce tearing, bulging, edge distortion, and unwanted movement around the bend termination. Relief width and depth should be evaluated together with material thickness, inside bend radius, bend angle, flange geometry, and the intended forming process.
Quick Overview
A sheet metal bend relief separates the material being bent from adjacent areas that should remain flat. As a practical design principle, relief width is usually related to sheet thickness, while relief depth should extend beyond the active bend region.
Rectangular, rounded, slit, and corner reliefs are commonly used. The correct geometry depends on the material, bend radius, cutting method, nearby features, assembly requirements, and the final shape of the part.
This sheet metal bend relief guide explains when relief is needed, how width and depth should be considered, and what engineers should check before releasing a design for production.
What Is a Sheet Metal Bend Relief?
A sheet metal bend relief is an intentional cut made where a bend line terminates. During bending, the outside of the material stretches while the inside is compressed. When a bend runs from one free edge to another, the sheet often has enough freedom to accommodate this deformation.
Problems are more likely when the bend stops inside the part or ends beside another flange or flat section. Material near the termination can be pulled into the bend zone, creating localized stress and distortion.
The relief creates separation between the forming area and neighboring material. This allows the flange to bend more independently and helps preserve the geometry around the bend.
For complex formed components, bend relief should be reviewed as part of the complete flat pattern rather than as an isolated CAD feature. JUSHUN's DFM engineering and design support focuses on identifying these manufacturability issues before production.
When Is Bend Relief Needed?
A sheet metal bend relief is most useful when nearby material restricts movement at the end of a bend.
A typical example is a partial flange that stops before reaching the end of a larger panel. As the flange is formed, the transition area can stretch unevenly because the bent section is still connected to material that should remain flat.
The same issue appears in brackets, chassis, cabinets, covers, and equipment enclosures. Where two flanges meet at a corner, each bend can influence the surrounding material. Without enough clearance, the corner may bulge, overlap, or require manual correction after forming.
Tabs and narrow formed sections may also need relief because they are often surrounded by material on both sides.
Not every bend requires a separate relief. If the bend runs completely from one free edge to another and surrounding material does not restrict deformation, an additional relief may provide little benefit. The key design question is whether the material around the bend termination has enough freedom to form without damaging nearby geometry.
Sheet Metal Bend Relief
Why Bend Relief Prevents Tearing and Distortion
During press brake forming, material throughout the bend zone stretches, compresses, and shifts. At the end of a partial bend, deformation can become concentrated because the bent section remains connected to adjacent material.
If the geometry is too restrictive, stress can build at the bend termination. The result may be a small tear, warped edge, uneven corner, or movement in a nearby feature.
This can also affect dimensional accuracy. A hole, slot, tab, or mating edge located too close to the bend may shift during forming and create assembly problems later.
A properly designed sheet metal bend relief gives the material a controlled area in which to deform. It does not remove forming stress, but it reduces the amount of unwanted force transferred into surrounding features.
Common Types of Sheet Metal Bend Relief
Different relief geometries suit different manufacturing conditions and final part requirements.
Rectangular Bend Relief
A rectangular relief uses a straight-sided slot extending beyond the bend zone. It is simple to design, easy to produce by laser cutting, and widely used in brackets, panels, covers, and cabinets.
https://www.jushunmetal.com/precision-sheet-metal-laser-cutting/
Its main limitation is the sharper internal corner at the end of the cut, which can create a more concentrated stress transition than a rounded design.
Rounded Bend Relief
A rounded relief uses a radiused end instead of a sharp termination. This creates a smoother transition and may be preferred where vibration, repeated loading, or leak initiation is a concern.
It can also provide a cleaner appearance where the relief remains visible after assembly.
Slit Relief
A narrow slit can be used where available space is limited. It removes less material, but the opening still needs to provide enough separation for the forming process.
A slit that looks acceptable in CAD may not perform well if it is too narrow for the cutting method or does not provide enough clearance during bending.
Corner Relief
Corner relief is used where two or more bent flanges intersect, especially in enclosure and box-type parts.
The final geometry depends on what happens after forming. A welded cabinet may require a different corner treatment from a removable cover where gap control, sealing, and appearance are more important.
How Wide Should a Sheet Metal Bend Relief Be?
The width of a sheet metal bend relief should normally be considered in relation to material thickness rather than selected as an arbitrary fixed value.
As a practical starting point, many fabrication guidelines use a relief width approximately equal to or slightly greater than the sheet thickness. The final value still depends on material type, cutting process, bend geometry, and the minimum feature size that can be produced reliably.
If the relief is too narrow, it may not provide enough separation for the material to deform freely. If it is unnecessarily wide, it can create visible gaps, reduce local stiffness, complicate welding, or affect sealing.
The correct width is therefore the amount of clearance needed for reliable forming without compromising the function of the finished part.
How Deep Should a Bend Relief Be?
Relief depth determines whether the cut reaches far enough into the bend area to release the material.
If the relief stops inside the active bend zone, the surrounding material may remain constrained. Tearing or distortion can still occur even though a relief has technically been added.
For this reason, sheet metal bend relief depth should be evaluated together with material thickness and inside bend radius. A practical DFM approach is to extend the relief beyond the effective bend zone rather than stop directly at the theoretical bend line.
There is no single depth that applies to every sheet metal component. Material type, thickness, bend radius, bend angle, tooling, flange geometry, and nearby features all influence the required value.
Bend Relief and Bend Radius
A sheet metal bend relief and the inside bend radius should be designed together because the radius affects the size of the deformation zone.
A tighter bend concentrates deformation more strongly, while a larger radius spreads it across a wider area. Material thickness and alloy also influence how the sheet behaves as it forms.
If the relief does not extend beyond the area affected by the bend, nearby material can remain partially constrained.
Material Thickness + Inside Bend Radius + Bend Angle + Flange Geometry + Nearby Features
These factors should be considered together before the flat pattern is approved.
For more information on forming considerations, see JUSHUN's CNC bending and sheet metal forming capabilities.
https://www.jushunmetal.com/cnc-bending-sheet-metal-forming/
Bend Relief vs. Corner Relief
Bend relief and corner relief are related, but they solve slightly different problems.
A bend relief primarily releases material where one bend terminates. A corner relief manages the intersection between two or more bent flanges.
For a partial flange, the main concern may be the bend termination itself. For a four-sided enclosure, the designer must also consider flange overlap, welding access, corner gaps, sealing, assembly fit, and final appearance.
The correct solution therefore depends on what the finished corner must do, not only on how the flat pattern looks before forming.
Features Near the Bend Zone
Holes, slots, cutouts, tabs, threaded hardware, and mating edges can all move or distort if they are positioned too close to a bend.
A sheet metal bend relief can reduce local stress, but it cannot compensate for every poorly positioned feature.
A hole close to the bend may elongate. A narrow tab may twist. A mating edge may move enough to affect final assembly. In these cases, changing feature location can be more effective than simply increasing relief size.
The complete geometry should therefore be reviewed together. Feature position, edge distance, flange width, material thickness, bend radius, and final tolerance all influence the manufacturing result.
Common Bend Relief Design Mistakes
One of the most common mistakes is making the relief too short. If the cut ends inside the active bend zone, the surrounding material can remain constrained and the original distortion problem may continue.
A relief that is too narrow can also be ineffective, especially when the sheet is relatively thick or the cutting process cannot reproduce the feature consistently.
The opposite problem is an oversized relief. Extra clearance may simplify bending, but it can also create an unnecessary opening that affects welding, sealing, appearance, or local strength.
Sharp internal relief corners deserve attention as well. They may be acceptable in many static applications, while rounded terminations can provide a smoother stress transition where vibration or repeated loading matters.
Another mistake is applying the same rule to every material. Mild steel, stainless steel, and aluminum do not behave identically during forming. Thickness, material condition, bend direction, tooling, and radius all affect the result.
A useful sheet metal bend relief guide should therefore provide design principles rather than present one universal dimension as correct for every part.
Bend Relief in Prototype and Production Parts
A prototype can sometimes appear acceptable even when its sheet metal bend relief geometry is marginal.
During a small run, an experienced operator may compensate for a difficult bend or manually correct minor distortion. That does not necessarily mean the design is suitable for repeat production.
As quantities increase, bend angle, flange position, corner appearance, assembly fit, and inspection results need to remain consistent without depending on repeated manual correction.
A properly designed relief helps create a more predictable forming process and reduces unnecessary variation between parts.
This is particularly important for equipment enclosures, electrical cabinets, control boxes, brackets, covers, chassis, and other OEM products where several formed components must fit together accurately.
What Should Engineers Check Before Production?
Before releasing a design, engineers should confirm where every bend starts and stops and whether nearby material restricts the forming zone.
A sheet metal bend relief should extend far enough beyond the active bend area, while its width should suit the material thickness and manufacturing process. Nearby holes, slots, tabs, hardware locations, and mating edges should also be checked for possible distortion.
The finished assembly should be evaluated at the same time. If the part will later be welded, sealed, mechanically assembled, or used as a visible exterior component, the relief geometry needs to support those downstream requirements.
For buyers working with an external fabrication partner, bend relief is only one part of supplier evaluation. JUSHUN's guide to sheet metal contractors, capabilities, and supplier selection explains what to consider when comparing manufacturers for drawing-based projects.
Conclusion
A sheet metal bend relief gives material room to deform where a bend terminates and helps reduce tearing, bulging, edge distortion, and unwanted movement around nearby features.
The correct geometry depends on material thickness, inside bend radius, bend angle, tooling, flange geometry, feature location, and final assembly requirements. Width should provide enough separation for forming, while depth should extend beyond the effective bend region.
There is no universal relief dimension for every part. For production designs, bend relief should be reviewed together with the complete forming geometry before the flat pattern is released.
For projects involving cutting, bending, welding, finishing, and assembly, you can also review JUSHUN's sheet metal fabrication capabilities.
Need a DFM Review for Your Sheet Metal Part?
If you already have 2D drawings or 3D CAD files, JUSHUN can review bend geometry, relief design, material, thickness, tolerances, and other forming considerations before quotation.
A DFM review can help identify bend-related risks before the flat pattern is released for cutting and production.
Send Your Drawings https://www.jushunmetal.com/contact/
Review DFM Support https://www.jushunmetal.com/dfm-engineering-design-support/
"B26, Huachuang Industrial Park, Guangzhou, China
tina@jushunmetal.com
Phone
+86 153 6005 0907
+86 153 6005 0907
Website https://www.jushunmetal.com/
B26, Huachuang Industrial Park, Guangzhou, China
tina@jushunmetal.com
Phone
+86 153 6005 0907
+86 153 6005 0907
Website
https://www.jushunmetal.com/ "
This release was published on openPR.
Permanent link to this press release:
Copy
Please set a link in the press area of your homepage to this press release on openPR. openPR disclaims liability for any content contained in this release.
You can edit or delete your press release Sheet Metal Bend Relief: Types, Design Rules and Size Guidelines here
News-ID: 4619716 • Views: …
More Releases from Jushun
Can You Jump Start a Hybrid
Can you jump start a hybrid when it will not switch on? Often, yes-if a discharged 12V auxiliary battery is preventing startup and the manufacturer permits external assistance. A compatible power source can help activate the electronics and hybrid control system.
https://www.delbestpower.com/blog/can-you-jump-start-a-hybrid/
Normal jump starting supports the low-voltage system. It does not recharge the high-voltage traction battery or repair a hybrid-system fault.
Quick Overview
Many hybrids accept a compatible 12V jump starter. Use the…
Aluminum Sheet Metal Enclosure: 5052 vs 6061
An aluminum sheet metal enclosure combines low weight, corrosion resistance, and good fabrication potential, but the alloy must match the manufacturing process.
https://www.jushunmetal.com/blog/aluminum-sheet-metal-enclosure/
5052-H32 is better suited to enclosure bodies with multiple bends. 6061-T6 provides higher strength and better machinability but requires more careful bend design. The material decision also affects welding, finishing, hardware installation, and final assembly.
For OEM projects, choose the alloy according to the complete enclosure-not strength alone.
Quick Overview
Use 5052-H32…
Custom Metal Enclosure Services
OEM equipment manufacturers rarely need only a cut and bent metal box. A production enclosure may also require drawing review, welding, surface finishing, hardware installation, assembly, and inspection, with each stage affecting the next.
https://www.jushunmetal.com/blog/custom-metal-enclosure-services/
JUSHUN has provided custom metal enclosure services since 2005. Our role is to help turn drawings, 3D files, BOMs, and project specifications into manufacturable enclosures, then maintain the approved geometry, finish, hardware interfaces, and assembly fit as…
How to Jump Start a Motorcycle Safely
A weak battery can leave a motorcycle unable to start even when the rest of the bike is working normally. Knowing how to jump start a motorcycle safely helps restore enough starting power without creating unnecessary risk to the battery, electrical system, or jump starter.
https://www.delbestpower.com/blog/jump-start-a-motorcycle/
The key is simple: confirm the correct voltage, inspect the battery, make the connections carefully, use short starting attempts, and disconnect the equipment in the correct…
More Releases for Bend
Fort Bend Hearing Recognized as Best Audiologist in Fort Bend County for 2025
Image: https://www.globalnewslines.com/uploads/2026/03/1774370268.jpg
Sugar Land, TX - Fort Bend Hearing has been named Best Audiologist in Fort Bend County for 2025 by Living Magazine as part of its annual "Best Of - Readers' Choice Awards," a community-driven recognition program that highlights local businesses based on public voting.
The Living Magazine Readers' Choice Awards are determined by votes from residents across the region, reflecting the preferences and experiences of the local community. This recognition…
Bend or Break: From Empires to Algorithms
ISBN: 979-8266536050
FOR IMMEDIATE RELEASE
1st October 2025
Newly-published: Bend or Break: From Empires to Algorithms - Lessons from History on How to Make Today's Societies More Resilient
About the book:
Why do some societies crumble under pressure while others rise stronger?
What can the past teach us about surviving the shocks of the future?
And how can humanity adapt in the age of AI?
From the fall of empires to the dawn of algorithms,…
Cut And Bend Equipment Market Size Analysis by Application, Type, and Region: Fo …
According to Market Research Intellect, the global Cut And Bend Equipment market under the Internet, Communication and Technology category is expected to register notable growth from 2025 to 2032. Key drivers such as advancing technologies, changing consumer behavior, and evolving market dynamics are poised to shape the trajectory of this market throughout the forecast period.
Due to the growing need for accurate and efficient steel processing in the construction industry, the…
Bend Insensitive Fiber Market - Industry Trends and Forecast to 2032
𝐓𝐡𝐞 𝐠𝐥𝐨𝐛𝐚𝐥 𝐁𝐞𝐧𝐝 𝐈𝐧𝐬𝐞𝐧𝐬𝐢𝐭𝐢𝐯𝐞 𝐅𝐢𝐛𝐞𝐫 𝐦𝐚𝐫𝐤𝐞𝐭 𝐰𝐚𝐬 𝐯𝐚𝐥𝐮𝐞𝐝 𝐚𝐭 𝐚𝐩𝐩𝐫𝐨𝐱𝐢𝐦𝐚𝐭𝐞𝐥𝐲 𝐔𝐒𝐃 𝟏𝟑.𝟑𝟓 𝐛𝐢𝐥𝐥𝐢𝐨𝐧 𝐢𝐧 𝟐𝟎𝟐𝟑 𝐚𝐧𝐝 𝐢𝐬 𝐩𝐫𝐨𝐣𝐞𝐜𝐭𝐞𝐝 𝐭𝐨 𝐫𝐞𝐚𝐜𝐡 𝐚𝐫𝐨𝐮𝐧𝐝 𝐔𝐒𝐃 𝟐𝟑.𝟔𝟒 𝐛𝐢𝐥𝐥𝐢𝐨𝐧 𝐛𝐲 𝟐𝟎𝟑𝟐, 𝐰𝐢𝐭𝐡 𝐚 𝐜𝐨𝐦𝐩𝐨𝐮𝐧𝐝 𝐚𝐧𝐧𝐮𝐚𝐥 𝐠𝐫𝐨𝐰𝐭𝐡 𝐫𝐚𝐭𝐞 (𝐂𝐀𝐆𝐑) 𝐨𝐟 𝐚𝐩𝐩𝐫𝐨𝐱𝐢𝐦𝐚𝐭𝐞𝐥𝐲 𝟔.𝟓𝟓% 𝐝𝐮𝐫𝐢𝐧𝐠 𝐭𝐡𝐞 𝐟𝐨𝐫𝐞𝐜𝐚𝐬𝐭 𝐩𝐞𝐫𝐢𝐨𝐝.
𝐁𝐞𝐧𝐝 𝐈𝐧𝐬𝐞𝐧𝐬𝐢𝐭𝐢𝐯𝐞 𝐅𝐢𝐛𝐞𝐫 𝐌𝐚𝐫𝐤𝐞𝐭 𝐎𝐯𝐞𝐫𝐯𝐢𝐞𝐰
The bend insensitive fiber market is witnessing steady growth due to increasing demand for high-speed data transmission and reliable connectivity solutions. These fibers are designed to…
Demand Analysis of Cut and Bend Equipment Market from 2027
Cut & bend equipment has numerous applications in the construction industry based on its different shapes, size, and quantities. Cut & bend equipment is used for cutting and bending purposes. The equipment helps in managing the inventory better which not only reduces the space requirement for keeping the rebars but also assists in saving costs associated with labor and wastage. Demand for integrated equipment for reinforcing processes is expected to…
Global Bend Fixtures Market Analysis by 2020-2025
Scope of the Report:
The global Bend Fixtures market size is expected to gain market growth in the forecast period of 2020 to 2025, with a CAGR of xx%% in the forecast period of 2020 to 2025 and will expected to reach USD xx million by 2025, from USD xx million in 2019.
Market segmentation
Bend Fixtures market is split by Type and by Application. For the period 2015-2025, the growth among segments…